я. Material Overview & Standardization
C75S is a high-carbon, non-alloy spring steel standardized under the German DIN EN 10132-4 specification. It corresponds to Chinese GB/T 75, American AISI 1075, and Japanese JIS S75CM standards. Its core characteristics are a high elastic limit and excellent fatigue resistance. Under comparable surface conditions and full hardenability, its fatigue limit can match some alloy spring steels. As a typical non-alloy spring steel, C75S achieves a balance of strength and toughness through precise control of carbon content (0.70%-0.80%) and impurity elements (P鈮?.025%, S鈮?.025%). It is particularly suitable for manufacturing small-to-medium-sized spring components.
II. Химический состав & Механические свойства
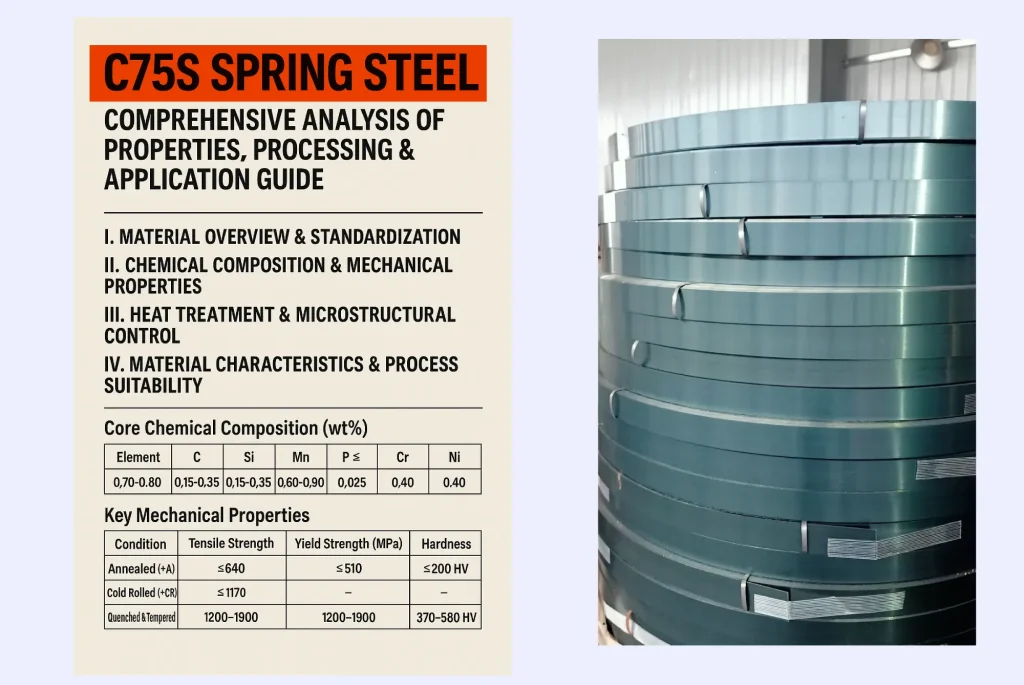
- Core Chemical Composition (wt%)
| Элемент | С | И | Мин. | P鈮?/th> | S鈮?/th> | Cr鈮?/th> | Ni鈮?/th> | Mo鈮?/th> |
|---|---|---|---|---|---|---|---|---|
| Content | 0.70-0.80 | 0.15-0.35 | 0.60-0.90 | 0.025 | 0.025 | 0.40 | 0.40 | 0.10 |
Source: DIN EN 10132-4:2000
- Key Mechanical Properties
| Состояние | Предел прочности (МПа) | Предел текучести (МПа) | Удлинение (%) | Твердость |
|---|---|---|---|---|
| Отожженный (+А) | ниобий?40 | ниобий?10 | ниобий?5 | ниобий?00 HV |
| Холод катился (+CR) | ниобий?170 | – | – | ниобий?20 HV |
| Закаленный & Закаленный (+QT) | 1200-1900 | – | – | 370-580 HV |
Примечание: Закаленный & Tempered hardness corresponds to HRC 38-55, depending on tempering temperature.
III. Термическая обработка & Microstructural Control
- Typical Heat Treatment Sequence
- Отжиг: 680-710掳C, furnace cooled. Relieves machining stress, produces pearlite + ferrite structure, hardness 鈮?00 HV, facilitating cold working.
- закалка: 780-820掳C, oil or water quenched. Austenitization followed by rapid cooling forms martensite, achieving hardness of 60-64 СПЧ. (Oil quenching reduces distortion/cracking risk; water quenching suitable for thin sections).
- Закалка: 180-300掳C, hold 1-3 hours. Adjusts hardness to 38-55 СПЧ, relieves internal stresses, forms tempered troostite structure, enhancing elastic stability.
- Process Innovation Case Study
- C75S strip for retaining rings achieved 鈮rade 7 grain size and decarburization layer 鈮?.06mm via clean steelmaking (LF + RH refining, inclusion rating 鈮?.0) and controlled rolling/cooling (finishing temperature 鈮?00掳C, coiling temperature 鈮?50掳C). After quenching and tempering, hardness reached 53-58 СПЧ, meeting high-end requirements for fatigue life (1 million cycles without cracking).
IV. Material Characteristics & Process Suitability
- Core Advantages
- Cost-Effectiveness: Lacks expensive alloying elements.
- Обрабатываемость: Annealed state allows stamping and bending. Cold-rolled strip achieves tight thickness tolerances (卤0.008mm), ideal for precision parts.
- Качество поверхности: Cold-rolled surface roughness Ra鈮?.8渭m, often eliminating the need for additional polishing for spring applications.
- Limitations
- Limited Hardenability: Oil quenching effective diameter 鈮?2мм. Large sections require water-oil quenching.
- Poor Weldability: Preheating 鈮?00掳C required before welding; post-weld stress relief annealing at 600掳C necessary.
В. Application Areas & Case Studies
- Key Application Fields
| Sector | Typical Products | Key Performance Requirements |
|---|---|---|
| Автомобиль | Clutch diaphragm springs, brake springs | Tensile strength 鈮?400МПа, Fatigue limit 鈮?00МПа |
| Precision Machinery | Watch mainsprings, instrument hairsprings | Elastic modulus 210GPa, Permanent set 鈮?.1% |
| Tool Manufacturing | Hand saw blades, cutting blades | Твердость 52-55 СПЧ, Excellent edge wear resistance |
| Appliances | Washing machine damper springs, printer pressure springs | Stress relaxation rate 鈮?% (150掳C 脳 1000h) |
- Innovative Application Case
- In new energy vehicle battery packs, laser-welded C75S strip, tempered at low temperature, forms battery compression springs. Precise hardness control (42-45 СПЧ) and flatness (ниобий?.15мм) ensure uniform pressure (200-300N) on battery cells while maintaining stability across temperature cycles (-40掳C to 125掳C).
VI. Performance Comparison with Competing Materials
| Свойство | C75S (ОТ 1.1248) | 65Мин. (GB/T 1222) | 55SiCr (В 10089) |
|---|---|---|---|
| Carbon Content | 0.70-0.80% | 0.62-0.70% | 0.51-0.59% |
| Предел текучести (QT) | 1200-1600 МПа | 1100-1500 МПа | 1300-1700 МПа |
| Fatigue Limit | 550-650 МПа | 500-600 МПа | 650-750 МПа |
| Hardenable Dia. (Oil) | ниобий?2 мм | ниобий?0 мм | ниобий?0 мм |
Заключение: C75S offers outstanding cost-performance for small-to-medium springs, matching 65Mn performance while offering significant cost advantages over 55SiCr.
VII. Selection & Application Guidance
- Specification Guide
- Cold-Rolled Strip: Thickness 0.15-2.0mm. Ideal for precision springs, лезвия.
- Hot-Rolled Plate: Thickness 2.0-20mm. Used for large dies, mechanical parts.
- Cold-Drawn Wire: Diameter 1.0-10.0mm. For coil springs, часовые пружины.
- Quality Control Essentials
- Decarburization Check: Critical springs require total decarb depth 鈮?% of thickness (например, ниобий?.005mm for 0.5mm strip).
- Non-Metallic Inclusions: Use ultrasonic inspection (鈮rade 2 per GB/T 10561) to avoid premature failure from Type B inclusions.
- Hardness Uniformity: Batch hardness variation should be 鈮? СПЧ.
VIII. Industry Trends & Technological Outlook
- Microalloying Enhancement: Adding 0.02-0.05% Nb refines grain structure, potentially increasing tensile strength by 8-12%, enabling use in larger springs.
- Green Manufacturing: Direct rolling of continuous cast slabs (CC-HDR) reduces energy consumption by 15% and CO鈧?emissions by 20%.
- Surface Coating Technology: PVD Cr coating or nitriding increases surface hardness to >800 HV, improving wear resistance by 30%, suitable for corrosive environments.
Заключение
C75S spring steel maintains an indispensable position in small-to-medium springs and precision cutting tools due to its balanced properties, controlled cost, and broad process adaptability. Driven by automotive lightweighting and smart manufacturing, material-process-design integration will likely unlock new applications in emerging fields like new energy and robotics. Engineers are advised to prioritize cold-rolled thin-gauge products to leverage their high precision and surface quality, while emphasizing supplier clean steelmaking capabilities to ensure consistent material performance.